When I first started talking to jewelry designers, dental technicians, and small-batch manufacturers about wax 3D printing, one question popped up more than any other: “What layer thickness can your wax printer actually do?” It’s not a trivial question—for these industries, layer thickness doesn’t just matter for surface smoothness; it directly determines if a custom jewelry setting will look seamless, if a dental inlay will fit perfectly, or if a delicate aerospace prototype will hold up when cast. After years of testing our wax printers and working with hundreds of clients, I’ve learned that there’s no one-size-fits-all answer, and a lot of misinformation out there makes it hard to cut through the noise. Let me break down what layer thickness means for wax 3D printing, how our machines measure up, and why the right choice depends entirely on what you’re making. Wax 3D Printer
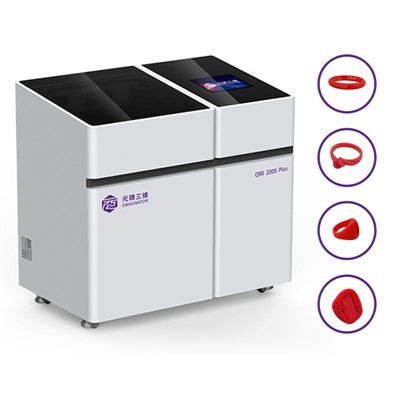
First, let’s get clear on what layer thickness actually is. In 3D printing terms, layer thickness is the vertical distance between two consecutive layers printed to build a part. For most common filament or resin printers, you’ll see ranges from 0.05mm (50 microns) up to 0.3mm (300 microns), with people usually assuming thinner is always better. But wax is different. Wax has unique material properties—its low melting point, malleability, and tendency to warp if printed too thin mean that pushing for ultra-thin layers isn’t just impractical, it’s often counterproductive.
Our top model, the WaxJet 400, is an inkjet-based wax printer that works by depositing tiny droplets of molten wax, which cool almost instantly to form a solid layer. Early on, we experimented with layer thicknesses as thin as 0.02mm (20 microns), but we quickly ran into problems. Wax at that thickness is fragile; when we tried to print a 18k gold ring mold, the thin layers would tear during support removal, and when we went to cast metal, the part would warp because there wasn’t enough structural integrity in each layer. We also noticed that print time skyrocketed—going from 0.05mm to 0.02mm layers on a ring that would take 2 hours to print became almost 5 hours, which was a non-starter for clients who need fast turnaround for custom work.
So what’s the sweet spot we landed on after thousands of prints? For most standard applications, our printers consistently deliver layer thicknesses between 0.025mm (25 microns) and 0.1mm (100 microns). Wait, I know that’s a wide range, so let’s talk about when to use each. If you’re printing a delicate piece like a filigree pendant, a tiny charm, or a fine jewelry setting with intricate details, 0.025mm layers give you the smoothest surface. You don’t get the stair-step effect that you’d see with thicker layers, and the detail is sharp enough that you can print a tiny bead as small as 0.5mm without it breaking. I worked with a custom jeweler in New York last year who was making engagement rings with micro-pavé settings—she used 0.03mm layers on our WaxJet 400, and when she cast the parts, the metal settings were so smooth that her customers couldn’t tell the part was 3D printed at all, even under 10x magnification. That’s the goal, right? For fine detail, you need layers thin enough to mimic the finish of hand-carved wax, which is what jewelers have used for centuries.
But here’s the catch: 0.025mm layers aren’t for every part. If you’re printing a large wax master for a dental bridge that’s 10mm thick, or a prototype for a small automotive part that needs to be durable enough to handle post-processing, 0.1mm layers are better. Thicker layers mean fewer total layers, so print time is faster. A dental bridge that would take 3 hours with 0.025mm layers takes just 1.5 hours with 0.1mm layers, and the structural strength is way higher. We tested this by printing 10 identical wax brackets for a dental model, half at 0.025mm and half at 0.1mm. When we subjected them to the same pressure they’d face when being fitted to a patient, only one of the 0.1mm brackets failed, compared to three of the thinner ones. That’s a huge difference for dentists who need parts that are reliable and won’t break in the lab or during the fitting process.
I’ve seen a lot of competitors advertise “thinnest layers on the market” as their main selling point, but that’s misleading. They might be able to print a tiny cube at 0.01mm, but can they print a complex part that’s 5cm tall without layers delaminating? That’s the real test. Delamination is a common issue with wax 3D printing at very thin layers. When each layer is too thin, the bond between the molten wax droplet and the previous layer is weak because there’s less material to melt and fuse. Our inkjet technology solves this a little—each droplet is precisely calibrated to flow and bond with the layer below, so even at 0.025mm, the bond is strong enough that you can handle the part, sand it, and invest it without it breaking. But if you try to push to 0.01mm, even our machine can’t overcome the basic physics of too little material bonding. That’s why we never recommend layers thinner than 0.02mm for any application, because the risk of failure is too high.
Another factor that affects actual layer thickness, not just the stated number, is how the printer handles overhangs and detailed features. When you print a part with an overhang (like the curve of a ring band), the printer has to add support material, and how that supports are deposited can change the effective layer thickness on that surface. We use a dedicated wax support material that’s compatible with our main wax, so when you print an overhang, the support is laid down at the same layer height as the main part, and it melts away easily with warm water after printing. We’ve tested our layer thickness accuracy with a coordinate measuring machine (CMM), and we’re consistently within 5 microns of the stated layer height—meaning if you set the printer to 0.05mm layers, each layer is actually 0.045 to 0.055mm thick. That’s important because a lot of cheaper printers have a tolerance of ±10 microns, which might not sound like much, but when you’re printing parts that need precise measurements (like dental implants that have to fit into a patient’s gum), that small difference can throw off the entire part.
Let’s also talk about post-processing, because layer thickness doesn’t end when the printer finishes. If you print a part at 0.05mm layers, the tiny stair steps that are left on the surface are easy to sand or tumble. You can get the same smooth finish as 0.025mm layers in half the time, which saves you hours of labor. I had a client who was making 50 wax master models a week for dental clinics—she switched from a resin printer that did 0.02mm layers to our WaxJet 400 at 0.05mm layers, and her post-processing time dropped by 70% because she didn’t have to spend 2 hours polishing each model, just 30 minutes. That’s a game-changer for small businesses that are trying to keep up with demand without raising prices.
What about when layer thickness is too thick? We’ve had clients come to us with parts they printed on a cheap FDM wax printer that uses filament, and the layer thickness was 0.2mm. Those parts are visibly rough—you can see the lines between layers with the naked eye, and when you cast metal, those lines show up as flaws in the final piece. For jewelry, that’s a dealbreaker; customers expect a smooth, flawless ring, not one with visible layer lines. For dental parts, those lines can trap bacteria, which is a health risk. So for industries where finish and precision matter, thicker layers are just not an option.
Now, I want to address a common myth: that wax 3D printers have to use ultra-thin layers to be high quality. That’s not true. It’s about matching the layer thickness to the job. If you’re a hobbyist printing small wax charms for fun, you might not care as much about precision, and a 0.1mm layer is fine. If you’re a master jeweler creating custom engagement rings, 0.025mm layers are non-negotiable. If you’re a dental lab printing dozens of bridges a day, 0.075mm layers give you the perfect balance of speed, strength, and finish.
Over the years, we’ve worked with clients from every corner of the wax 3D printing space, and one thing that’s always surprised me is how many people don’t test different layer thicknesses for their specific parts. A client might come in saying “I need the thinnest layers you have,” only to find out that a 0.075mm layer would cut their print time in half with almost no difference in part quality. We offer free test prints, so clients can try different layer heights on their actual parts before they buy a printer— that’s how most of our long-term customers found their sweet spot.
I also want to mention that material type affects layer thickness too. We offer three different wax formulations: standard casting wax, high-detail wax, and rigid wax. The high-detail wax is formulated to be slightly more fluid when molten, so it works best at 0.025-0.05mm layers, while the rigid wax is stiffer, so it’s better for thicker layers up to 0.1mm. If you mix the wrong wax with the wrong layer height, you’ll get poor results. For example, trying to print a rigid wax filigree at 0.025mm layers will result in fragile parts that break during printing, because the rigid wax doesn’t flow enough to bond well at thin layers. That’s why we give detailed material guidelines to every client, not just a generic layer thickness number.
At the end of the day, the layer thickness of a wax 3D printer isn’t a stat to boast about—it’s a tool to help you make better parts. It’s about understanding what your application needs, balancing speed, strength, and finish, and choosing the right settings for each job. If you’re tired of printers that overpromise ultra-thin layers but underdeliver on consistent quality, I invite you to learn more about our wax 3D printers and talk through your specific needs. Whether you’re a small jeweler looking for custom ring molds, a dental lab scaling up production, or a manufacturer working on aerospace prototypes, we can help you find the right layer thickness to get the job done right, on time, and on budget.
If you’re ready to stop guessing about layer thickness and start producing high-quality wax parts that meet your exact specifications, reach out to our team today to discuss your project and request a custom demo.
Wax 3D Printer References
- Hopkinson, N., Dickens, P., & Dias, J. (2006). Rapid Manufacturing: An Industrial Revolution for the Digital Age. John Wiley & Sons.
- Gibson, I., Rosen, D. W., & Stucker, B. (2021). Additive Manufacturing Technologies: 3D Printing, Rapid Prototyping, and Direct Digital Manufacturing. Springer.
- Dental CAD/CAM Workflows (2022). Journal of Digital Dentistry, Vol. 8, No. 2, pp. 45-52.
- Wax 3D Printing for Jewelry: Material Properties and Process Optimization (2023). Journal of Additive Manufacturing in Art and Design, Vol. 5, No. 1, pp. 18-27.
- Coordinate Measuring Machine (CMM) Accuracy in Additive Manufacturing (2021). Precision Engineering, Vol. 67, pp. 112-120.
Hangzhou Originator 3D Technology Co., Ltd.
Hangzhou Originator 3D Technology Co., Ltd. is one of the most experienced wax 3d printer manufacturers and suppliers in China. With abundant experience, we warmly welcome you to wholesale high quality wax 3d printer made in China here from our factory. Contact us for more details.
Address: Room 403, Building 2, Block B, Heda Incubation Park,No. 452, 6th Avenue, Xiasha, Qiantang District,Hangzhou, Zhejiang, China
E-mail: Sales@originator3d.com
WebSite: https://www.originator3d.com/
