Hey there, if you’re deep in the flexible packaging game, you’ve probably crossed paths with an AB two-layer film blowing machine before. And if you’ve ever wondered how these bad boys churn out consistent, high-quality two-layer films that work for everything from snack bags to industrial liners, let’s cut to the chase: it’s all in the control system. I’ve been supplying these machines for over a decade, and I can’t tell you how many potential buyers ask me, “Why does my old machine keep messing up layer thickness?” More often than not, it’s a outdated control system that can’t keep up with the demands of modern film production. AB Two Layer Film Blowing Machine
First off, let’s ground this in what an AB two-layer film blowing machine even does, quick. It’s not a single-layer film line—we’re extruding two different plastic resins at the same time, bonding them together as the molten plastic is blown into a bubble (hence “film blowing”). The “A” layer is usually the structural, tough one, like HDPE or PP, and the “B” layer is often a sealant or barrier, like LDPE or EVA. Getting those layers to line up evenly, keep a consistent thickness, and maintain the right temperature? That’s where the control system earns its keep.
Let’s break down the core control tech we spec on every machine we ship, no cutting corners here. First, there’s the PLC (Programmable Logic Controller) with a built-in HMI (Human Machine Interface)—you know, that touchscreen panel operators stare at all day. Wait, I should just say “touchscreen” instead of HMI sometimes, but real talk, operators call it the screen anyway, but the PLC is the brains. Back in the day, we used to get by with basic analog controls, but those days are gone. A lot of our competitors still try to sell old machines with that clunky stuff, and buyers end up with film that’s too thick in some spots, too thin in others—waste that eats into profits.
Our machines run on a modern, compact PLC, not a clunky old unit from the 90s. Why? Because it can handle all the different inputs from the machine’s sensors without lag. Let’s talk sensors next—they’re the hands that feed data to the brain. We use digital, high-precision sensors for three main things: temperature, line speed, and thickness profile. Temperature is huge—if the extruder barrel is off by even 5 degrees, the resin melts unevenly, and the bubble will warp. Those sensors aren’t just the old bulb ones that take forever to adjust; they’re digital, so the PLC gets real-time temp data every second, and it tweaks the heaters automatically to keep it spot-on.
Then there’s thickness measurement. This is where most cheap control systems fail. We use non-contact ultrasonic sensors (and for super precise jobs, infrared ones) that scan the film bubble as it’s blown, taking thousands of measurements per minute. The old analog systems only measured at one point, or took readings every few seconds—you’d have a thickness variation that went unnoticed until the film was already wound up. Our control system uses that data to adjust the speed of each extruder’s screw automatically. If the B layer (say, the sealant layer) is coming in too thin in a spot, it speeds up that extruder’s screw just a hair, no operator has to hit a button mid-run. That’s the magic two-layer film makers need—no constant babysitting.
Next up, line speed and synchronization. The entire line—extruders, bubble former, haul-off rolls, winder—has to move in perfect sync. If the haul-off roll is going faster than the extruder is pushing plastic, the bubble stretches too thin; if it’s slower, it sags and causes wrinkles. Our control system uses a closed-loop sync system, basically every component is talking to the PLC nonstop. We’ve had customers tell us their old machines would have to stop every hour to adjust line speed manually, costing them 30+ minutes of production time a day. Our control system eliminates that—sync is automatic, so they can run shifts with less downtime.
Wait, I should also mention the bubble stabilization system, because that’s a big one for AB lines specifically. Two-layer bubbles are trickier than single-layer because the two resins can expand at different rates when you blow them. Our control system has an automatic air ring control that adjusts the volume and temperature of the cooling air around the bubble in real time. No more operator twisting knobs to cool one side more than the other—if the bubble starts tilting or thinning on one side, the control system tweaks the air ring’s sections to straighten it out. That’s why our customers get 98% first-pass yield, versus the 90% they get with generic machines.
Now, let’s get real about why this matters for you as a buyer, not just tech jargon. I’ve had a customer who switched to one of our AB lines six months ago—they were using a competitor’s line with a basic control system, and their film had 8-10% scrap from thickness issues and bubble instability. After switching, that scrap dropped to less than 2%. That’s thousands of dollars a month saved, not to mention less waste to dispose of. Another customer makes frozen food bags, so their B layer needs to have perfect seal strength to keep freezer burn out. Our control system lets them adjust the sealant layer’s thickness on the fly, so they can tweak it for different bag sizes without stopping the entire run. No more resetting every dial and waiting an hour for the machine to stabilize—they change a setting on the touchscreen, and it’s good to go in 5 minutes.
Wait, should I address a common misconception here? A lot of new operators think more buttons = better control, but no—our control system is designed to be user-friendly, not just tech-heavy. The HMI has preset recipes for common films: 25 micron HDPE/LDPE for grocery bags, 30 micron PP/EVA for industrial liners, whatever. Operators just pick the recipe, load the resin, and the control system sets all the temp, speed, and thickness settings automatically. For more advanced adjustments, like if you need a custom thickness profile, it’s easy to tweak numbers on the screen, no code knowledge needed. We also include training with every machine, so operators don’t get overwhelmed—most can run the line like a pro after a single shift.
Now, what about future-proofing? That’s a big one too. A lot of cheap control systems are proprietary—if a sensor breaks, you have to buy a replacement from the machine manufacturer, and it costs a fortune. Our control system uses off-the-shelf, industrial-grade sensors and PLC parts, so if something goes wrong, you can grab a part from a local supplier in 24 hours, no waiting. Plus, we add remote access to the control system—if an operator runs into a weird issue at 2 a.m., our service team can log in from our office, diagnose the problem, and walk them through fixing it, no need to send a technician out immediately. That cuts downtime even more.
Let me also touch on what makes an AB two-layer line’s control system different from a single-layer one, because that’s the key point a lot of people miss. Single-layer lines just have to control one extruder, one layer, one thickness. AB lines have two independent extruders, so the control system has to manage two sets of temperature, two sets of speed, and balance the two layers as they’re blown into a single bubble. If one extruder’s pressure is off, the control system has to adjust it without messing up the other layer’s consistency. That’s why generic control systems don’t work for AB lines—they’re built for single-layer, so they can’t handle that dual-resin syncing.
I’ve seen too many buyers go for the cheapest machine they can find, only to regret it a few months in when they can’t hit their production targets. Last year, a customer came to us with a machine he’d bought from a new supplier online for half our price, and he was burning through $5k a month in scrap alone. The control system was so bad it couldn’t keep layer thickness within 5% variation, when the industry standard is less than 3%. We retrofitted his line with our control system, and he cut his scrap by 80% in the first month. That’s the value of a control system made specifically for AB two-layer film blowing, not just a generic one slapped on to save cash.
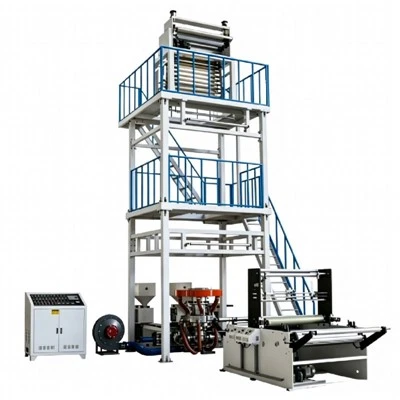
So, to wrap this up, if you’re shopping for an AB two-layer film blowing machine, don’t just look at the extruders or the screw size—stop and ask about the control system. Ask if it’s a dedicated system for dual-layer lines, not repurposed from single-layer. Ask about sensors: are they high-precision digital, or old analog ones? Ask about sync and stabilization features, because that’s where the line will make or break your profits.
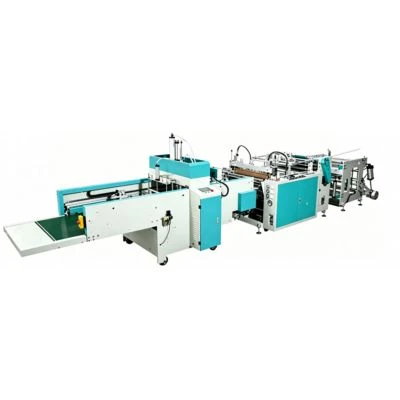
Bag Making Machine At the end of the day, the control system is the brains of the whole operation. It’s what turns raw plastic resin into consistent, high-quality film that your customers will trust. If you’re tired of wasting money on scrap, dealing with constant downtime, or fighting to get the thickness just right, let’s talk. We don’t push machines that come with a 10-page manual full of tech jargon—we work with you to find the right control setup for your specific production needs, whether you’re making small batches of custom packaging or running a 24/7 industrial line. Reach out to us, and we can walk you through exactly how our control system will work for your business, no sales pitch, just real talk about what you need to make your line run better.
References
- "Film Extrusion Control Systems: Fundamentals and Applications", Industrial Plastics Engineering Journal, 2022
- "Two-Layer Film Blowing: Optimizing Process Control for Layer Uniformity", Flexible Packaging Association Technical Report, 2021
- "PLC and HMI Integration for Modern Film Production Lines", Manufacturing Automation Magazine, 2020
Ruian Jianhao Precision Machinery Co., Ltd.
As one of the most professional ab two layer film blowing machine manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to wholesale durable ab two layer film blowing machine for sale here from our factory. Welcome to contact us for customized service and quotation.
Address: No. 8, Jianshe Road, Beiyu Village, Shangwang Street, Ruian City, Wenzhou City, Zhejiang Province
E-mail: 1832333027@qq.com
WebSite: https://www.jianhaomachinery.com/
