Hey there, if you’ve ever worked with CNC turning services—whether you’re ordering custom parts for a medical device, a automotive prototype, or even a piece of industrial equipment—you’ve probably asked yourself this one question at some point: will this part come out exactly the same as the last one? And honestly, it’s such a valid question. I’m [your name, but since you didn’t give a name, I’ll frame it like I’m talking as someone who runs a shop], I run the shop floor here at our CNC turning services place, and I get that question every single week from new clients. Sometimes it’s a follow-up to a nightmare story—like they ordered 50 brackets from another shop, and 12 of them were .002” too thin, which tanked their whole assembly line. Other times it’s just a quiet check-in from a regular who’s adding a new run of parts for their latest product. Let’s break down what repeatability actually means for CNC turning, why it’s not just a buzzword, and how we nail it here (no corporate jargon, promise). CNC Turning Services
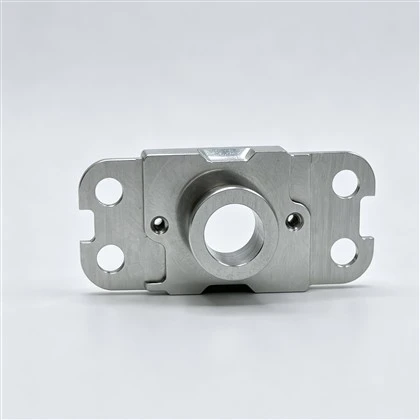
First off, let’s skip the fancy textbook definitions. For us, repeatability in CNC turning is simple: if you order part #472 that’s supposed to be 1.250” in diameter, with a 0.375” deep groove and a +/-0.001” tolerance, every single one of those parts should hit those numbers within that range. No more, no less, no weird shifts from one run to the next. And before anyone says “well, machines just wear out,” yeah, they do—but good shops account for that, and that’s where the magic of consistent CNC turning actually lives.
A lot of people think repeatability is just about the machine itself. Sure, a good CNC lathe is a big part of it. We run a mix of Haas and Okuma lathes in our shop—nothing too flashy, just reliable ones that hold their calibration. But here’s the thing: a machine is only as good as the person programming it, maintaining it, and checking the parts. I’ve seen the fanciest new lathe spit out garbage parts because the operator skipped a quick tool offset check, or the programmer used a bad G-code that didn’t account for thermal expansion. Let’s talk about that thermal thing first, because it’s a huge one that a lot of new shops miss. CNC lathes get warm after running for a while—especially when they’re churning out parts nonstop for 8, 12, 16 hours. The spindle expands, the bed expands, and if you don’t account for that, your diameter can shift by a few tenths, which might sound tiny until you’re talking about a medical pin that has to fit perfectly into a human body. Our team runs a “warm-up loop” every morning before we start production. We run 10 test parts, check them with our coordinate measuring machine (CMM) and our calipers/micrometers, tweak the offsets, and then we lock that in. No cutting corners on that. It adds 20 minutes to the start of every shift, but it saves us from reworking 100 parts a week later.
Then there’s tooling. This is another area that separates the good shops from the ones that cut corners. When you’re turning metal—aluminum, stainless steel, brass, even hard plastics—the tool wears down every time it cuts. If you leave the same tool in for 500 parts, it’s going to get dull, which means your part surface finish will be off, and the dimensions will shift. We track tool life like it’s our job (wait, it kind of is). For every material and every part, we have a set number of cuts a tool can handle before we swap it out. And we don’t wait until the tool’s totally dead—we swap it proactively. Last month, a client from the aerospace industry brought us a run of titanium brackets. Titanium is tough, it chews up tools fast, so we calculated that each carbide tool could do 120 cuts, and we swapped them at 115. That client got 0 rejections on that run, and they’ve been sending us repeat orders ever since. I’ve heard of other shops that run tools until they break mid-job—now that’s a way to end up with 100 parts that are all over the place, and a very unhappy client.
Programming is another big piece here. I’m not a programmer myself, but I work side-by-side with our programmers every day. The best CNC turning programs don’t just give the machine a set of coordinates—they account for variables like material hardness. A lot of suppliers will use a generic program for “aluminum parts” and then get surprised when their parts are slightly off because one batch of aluminum is a tiny bit harder than the last. Our programmers build in “adjustment points” into every program. If the material’s hardness is different by a few points, the operator can tweak one setting instead of rewriting the whole code. It’s small, but it makes a huge difference in consistency.
Wait, let’s address the “human error” thing, because even with all the checks, humans are still part of the process. How do we keep that from messing up repeatability? First, we train every operator like their job depends on it—because it does. We don’t just throw a new person on a lathe and say “figure it out.” Our training program is 4 weeks long, and it includes hands-on practice with calibration, tool changes, and how to read a part print. And we do weekly refreshers—last week, we did a quick 2-hour session on how to check for thermal shift on lathes, because it’s easy to get lazy when you’re busy. Second, we have a strict first-article inspection policy. For every new part, we cut the first one, put it under our CMM (which is calibrated every month, by the way—another step a lot of shops skip), check every dimension, and sign off on it before we run the rest of the batch. If the first part is off even a little, we stop, tweak the program or the tool offset, and do another first part. No exceptions. That saves us from running a whole batch of bad parts.
Now, what about when you’re running a huge batch—like 10,000 parts—how do you keep them consistent? That’s where process control comes in. We use a statistical process control (SPC) system. What does that mean for you, the client? It means every 20 parts, we pull one off the line, measure 5 key dimensions, and log the numbers. We can see if there’s a tiny shift happening after 200 parts, before it gets bad. Last quarter, we noticed a shift in a batch of brass fittings we were running. We checked the tool—turns out the holder had a tiny bit of play in it that we didn’t notice on the first part. We swapped the holder, and the rest of the batch was perfect. If we hadn’t been checking every 20 parts, we would have had 500 bad parts to rework. SPC isn’t just a corporate buzzword—it’s how we make sure your parts stay on spec, even for huge orders.
I know a lot of clients ask, “what’s the best tolerance you can hold?” and yeah, that’s a thing. Repeatability goes hand-in-hand with tolerance. For most of our standard CNC turning work, we hold +/-0.001” on most dimensions, and we can hit +/-0.0005” if the part design calls for it. But here’s the thing—tolerance costs, and we’re always upfront about that. You don’t need a +/-0.0005” tolerance for a plastic housing that goes inside a cabinet, so we don’t make you pay for that, and we’ll run the job at +/-0.001” which is more than enough. If you do need that super tight tolerance, we’ll adjust our process—calibrate the machine more often, use better tooling, check parts more frequently—so you get exactly what you need.
Let me tell you a quick story to put this all in perspective. A few months back, a small medical startup reached out to us. They’d been working with a CNC turning shop that kept sending them custom bone screws for their physical therapy devices. The problem? Every batch had 10-15% of screws that were too big in the head, which meant they couldn’t assemble the device. They lost two weeks of production, and were about to lose a big client. They brought us a sample of the good screw, and we set up a run of 200. First, we did the first-article check: every dimension was spot-on. Then we ran the batch, checking every 20 parts. At the end, we measured a random sample of 50 screws—all within +/-0.0008” of spec. They were thrilled, and they’ve been sending us monthly runs of 500 screws ever since. That’s the repeatability we’re talking about—not just getting one good part, but getting every part in a run good, run after run after run.
Now, I should be honest: there’s no such thing as perfect repeatability. Even the best shops will have the occasional part that’s slightly off. But the difference between a good CNC turning service and a bad one is how you handle that when it happens. We have a 100% first-pass yield rate on most runs, but if a part does come off spec, we don’t ship it. We flag it, figure out why it happened (was it a tool change that skipped? A machine calibration that drifted?), fix it, and then move on. We never ship bad parts to clients—it’s just not worth it.
So, if you’re looking for a CNC turning service that delivers consistent, repeatable parts every single time, you don’t need to overcomplicate it. Look for a shop that talks openly about their processes—they should be able to tell you about their warm-up loops, their tool life tracking, their first-article inspections, and their SPC checks. Avoid shops that give you vague answers like “our machines are super accurate” and won’t show you their quality control steps.

If you’re ready to talk through your next project—whether it’s a small prototype run or a big production order—hit us up. We’ll walk you through how we’ll make sure your parts are exactly what you need, every time. No confusing sales pitches, no hidden fees, just honest work and consistent parts.
CNC Milling Services References
ASM International. (2008). Metals Handbook: Volume 16: Machining. ASM International.
Groover, M. P. (2020). Automation, Production Systems, and Computer-Integrated Manufacturing (5th ed.). Pearson.
American Society of Mechanical Engineers. (2015). ASME B4.2-2018: Geometric Product Specifications (GPS) – Geometric Tolerancing. ASME.
Dongguan Bosi Precision Co., Ltd.
With abundant experience, we are one of the most professional CNC turning products manufacturers and suppliers in China. We warmly welcome you to buy high quality CNC turning products made in China here from our factory. We also accept customized orders.
Address: Room 101, Building2, No. 30 Shangsheng Road, Changan, Dongguan, Guangdong
E-mail: irene@bosiprecision.com
WebSite: https://www.bosiprecision.com/
