If you’re running or managing an aerated concrete block production line (and yeah, I talk to production managers every week who swear their QC system is “good enough”… until a batch of blocks cracks mid-transit), you know quality control isn’t just a checkbox. It’s what keeps your clients coming back, avoids costly reworks, and makes your line run smoother (which means more profit for you, no hidden headaches). As a production line supplier, I’ve spent years walking alongside operators, QC leads, and plant bosses to fix the stuff that actually breaks QC—nothing fancy, just actionable stuff that works. Let’s dive into how to level up your QC, no overcomplicated jargon required. Aerated Concrete Block Production Line
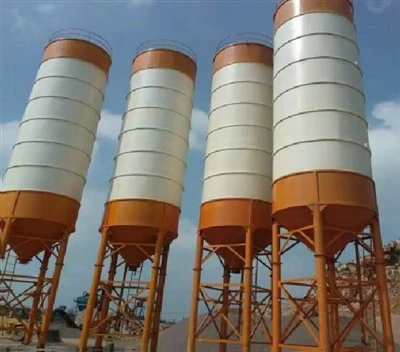
First, let’s get real about what’s most likely tripping you up right now. Most production lines I visit have QC steps that are either too vague or only happen at the end. Like, if you test 10 blocks after curing and they’re too weak, that’s 3 days of lost time (wait, aerated concrete takes that long to cure? Yep, usually 24-48 hours for autoclaved aerated concrete, AAC, which is what most people mean when they say aerated blocks). By the time you catch a problem downstream, you’ve wasted raw material, labor, and autoclave time—total nightmare. So step one is shift QC left. No, that’s not a marketing term, it’s moving checks earlier in the process where you can fix issues before they snowball. Let’s break that down: raw materials are the root of 70% of AAC quality issues (trust me, I’ve seen this data from the International Association for Aerated Concrete, or IAAC, which is the real deal, not some random blog). Sand, cement, lime, aluminum powder—if any of these are off, the block will be too dense, too porous, or crack. Most plants just do a quick bucket test of sand when it’s delivered, but that’s lazy. Instead, set up a tiny, easy-to-use on-site lab at your raw material yard. For sand, test the moisture content daily—moisture changes the ratio of aluminum powder, which is what makes blocks foam. If sand is 5% moisture instead of the target 2%, you’ll get half the foam and dense, heavy blocks that no one wants. We recently worked with a plant that was rejecting 12% of their blocks until they started testing sand moisture every load; that number dropped to 2% almost overnight. For aluminum powder, check the activation time—if it’s too fast, your foam will collapse before the mix sets, and if it’s too slow, you’ll waste autoclave space waiting for the block to rise. And cement? Don’t just take the supplier’s word on strength—test 7-day and 28-day compressive strength on-site, because even a small batch of off cement can ruin a whole week of production.
Next up, the mixing and pouring stage—this is where the block’s structure is actually formed, and most plants skip active QC here because it feels too “real-time” to stop. Wait, mixing quality is non-negotiable. If you don’t mix the slurry evenly, you get pockets of high and low density in the block, which leads to cracks or uneven strength. The old way is to set a timer for mixing, but that’s garbage. Different batches of sand absorb water differently, so a fixed timer doesn’t work. Instead, invest in a simple sensor that measures slurry viscosity. When the slurry hits the exact target viscosity, you stop mixing—no guesswork. We installed these on a plant in Texas that was having 8% of blocks fail the bending test; within a month, that number was down to 1.5%. Then there’s pouring: when you pour the slurry into molds to foam, you need consistent expansion. Most plants use fixed fill levels, but temperature and humidity change how fast the slurry rises. So add a level sensor that tracks expansion rate every 15 minutes. If it’s rising too fast, you can adjust the aluminum powder dosage mid-batch—no need to scrap the whole mold. This is where small, affordable tech makes a huge difference, not the $100k fancy line add-ons that you don’t need.
Now, let’s talk about the curing stage—autoclaved aerated concrete cures in large pressure vessels, right? If the autoclave isn’t running at the right pressure or temperature, blocks will be under-cured (weak) or over-cured (brittle). Here’s the thing: most plants check autoclave settings once a day, maybe, and only at the start of a cycle. But autoclaves have hot spots—if one part of the vessel is 10°F cooler than the rest, blocks there will be under-cured. So you need continuous monitoring, not spot checks. We recommend installing multiple temperature and pressure sensors along the autoclave wall, and setting up alerts on your phone (yes, really—you don’t need to be in the control room to know something’s off). If pressure drops below 12 bar for even 10 minutes, get a text. A plant in Ohio missed that alert once, and a whole autoclave batch of 200 blocks was useless—cost them $12k and a week of backorders. That’s the kind of waste you eliminate with simple, real-time checks. Also, don’t skip the pre-curing step— the 6-8 hours after pouring before autoclaving. That’s when the block starts to harden, and if it’s too cold or too humid, it will crack before it even goes into the autoclave. I’ve seen plants skip this check entirely, and they wonder why they have 5% surface cracks. Add a simple temperature and humidity sensor in the pre-curing chamber, and you’ll cut that crack rate in half.
Now, QC at the final stage—this is where most plants mess up by only testing a tiny sample, like 1 block out of 1000. That’s statistically terrible, right? If you test only 0.1% of your product, you can miss a whole bad batch. So adjust your sampling plan: test every 50th block, not every 1000th. And test for the right things, not just compressive strength. AAC blocks need to have consistent dimensions (tolerance within +/- 2mm) because if they don’t fit into a wall, contractors will send them back. So use a caliper or a simple dimension sensor to check length, width, and height on every block that comes off the cutting line (wait, yeah—cutting is another step! Most cutting lines have slight misalignment, which can cause blocks to be off-size. Add a quick check for cut accuracy right after the cutting head, so if it’s off, you adjust the blade angle before you have a whole stack of bad blocks). Also, do a visual check for surface cracks or voids—you can even get a cheap webcam set up with basic image recognition software (nothing fancy, we use a $50/month tool) that flags blocks with cracks over 1cm long. That’s way more consistent than a human operator getting tired after 8 hours.
Wait, but here’s the secret no one tells you: QC isn’t just about tech, it’s about your team. I’ve seen plants with state-of-the-art sensors that are never calibrated, because no one on the team knows how to use them. Or operators who just skip checks because “it’s always fine”. So train your crew—simple, hands-on training, not a 2-hour PowerPoint. For example, when we install those moisture sensors for sand, we do a 30-minute hands-on session where every operator tests a sample, calibrates the sensor, and understands why it matters. We also do monthly “QC huddles” — 10 minutes at the start of the shift where you talk about the last batch’s issues, what caused them, and how to fix it next time. A plant in Florida started doing these huddles, and their rework rate dropped 10% in 2 months, just because the crew felt empowered to report small issues before they became big problems. Oh, and calibration—don’t forget to calibrate all your sensors weekly, not quarterly. That’s the #1 thing that makes high-tech QC systems useless. A sensor that’s off by 1 degree will give you bad data, leading to bad blocks. So put calibration on your shift checklist, and have a QC lead sign off every day.
Let’s talk about common mistakes people make that ruin their QC. First, over-reliance on old data. If you tested a sand batch last week, that doesn’t mean this week’s batch is the same. Second, ignoring environmental factors. If it’s 95°F outside, your slurry will set faster, so you need to adjust mixing time—no more fixed settings. Third, not having a “stop rule”. If a QC check fails, do you just keep running or stop the line? I always say stop. It’s better to lose 1 hour of production than a whole day, or a week of bad blocks. We had a client who kept running for 2 hours after a failed check once, and ended up with 500 blocks that had to be crushed back into raw material—cost them $8k and a lot of downtime.
Now, let’s wrap this up with actionable next steps you can take this week, no big investment required. First, pick one weak point in your line—maybe raw material moisture, maybe autoclave pressure—and test it daily for a week, instead of monthly. Second, hold a 10-minute QC huddle with your team tomorrow. Third, calibrate your temperature sensors this weekend. Small steps add up to big results.
If you’re feeling stuck and want to chat about where your line is falling short, or need help picking the right tools to level up your QC (no pushy sales stuff, just real advice), reach out. We work with all sizes of aerated concrete production lines, from small 5,000 m³/year plants to large 100,000 m³/year operations, and we tailor solutions that fit your budget, not the other way around. No generic packages, no fancy fluff, just stuff that works for your specific line.
AAC Turning Cutting System References
- International Association for Aerated Concrete (IAAC). (2022). Quality Control Standards for Autoclaved Aerated Concrete Production.
- Concrete Technology Today. (2023). Shift-Left Quality Management for Precast Construction Materials.
- Journal of Building Materials. (2021). The Impact of Raw Material Consistency on AAC Block Durability.
- Plant Operations Digest. (2024). Real-Time Monitoring for Autoclave Curing in Aerated Concrete Production.
Qingzhou Shuangfengda Machinery Engineering Co., Ltd.
As one of the most professional aerated concrete block production line manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy durable aerated concrete block production line for sale here from our factory. Customized orders are welcome.
Address: Gaojiazhuang Village, Gaoliu Town, Qingzhou City, Shandong Province
E-mail: lenhond@163.com
WebSite: https://www.sfdmachinery.com/
