If you’ve ever worked in any industry that relies on rotating or load-bearing mechanical parts—whether that’s automotive, agricultural machinery, medical devices, or industrial robotics—you’ve likely had to specify CNC turned shafts. As someone who’s been supplying these precision-machined components for over 12 years, I’ve heard every question under the sun about them, but none come up as consistently as: “What’s the fatigue life of a CNC turned shaft?” CNC Turned Shafts
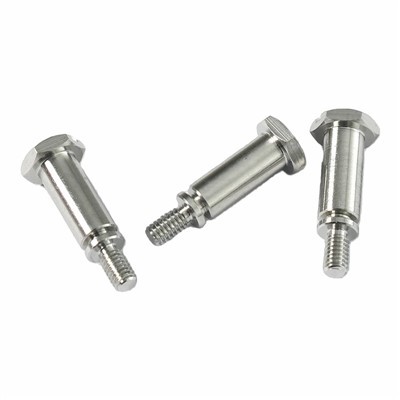
This isn’t a trivial question, by the way. Fatigue failure isn’t the dramatic, sudden break you might see in a movie; it’s a slow, insidious process where a tiny crack forms, grows incrementally over thousands or millions of cycles, and eventually leads to catastrophic breakdown. For a shaft, that could mean a $10,000 piece of custom machinery being sidelined for weeks, or worse, a safety hazard in a vehicle or medical device. So when a customer asks about fatigue life, they’re not just asking for a number—they’re asking for reliability, and I get that.
Let’s start with the basics, because a lot of folks assume all CNC turned shafts are the same, and that’s where the confusion begins. A CNC turned shaft isn’t just a metal rod with a fancy name. It’s a part that’s machined on a lathe with extreme precision—tolerances of 0.0001 inches, usually—from a specific material, with a specific surface finish, and finished with specific treatments. Every single one of these factors has a direct impact on fatigue life.
First, material selection. This is the foundation of any shaft’s fatigue performance. Most of the CNC turned shafts I supply are made from carbon steels (like 1045 or 4140), alloy steels (4340 is popular for high-load applications), stainless steels (303 or 316 for corrosion resistance), or sometimes specialty alloys like titanium for aerospace or medical use. Let’s talk about 4140 because it’s the workhorse for most general industrial applications. As a machinist, I can tell you that 4140 has a balance of strength, toughness, and machinability that’s hard to beat. Its fatigue limit—meaning the stress level below which it will never fail, no matter how many cycles it’s subjected to—is roughly 30,000 to 35,000 psi when in its quenched and tempered condition. That’s a pretty solid number, but it’s not universal. If you go to a higher-grade alloy, like 4340, the fatigue limit jumps to around 45,000 psi, but it’s more expensive and requires more careful machining to avoid defects.
Stainless steels are a different story. 303 stainless is easy to machine, which is why a lot of customers reach for it when they need corrosion resistance, but its fatigue limit is only about 20,000 psi. That’s a big drop, so I always have to warn customers: if your shaft is going to be under a repeated load, 303 might not be the right choice. 316 stainless is a bit better, around 25,000 psi, but still way lower than 4140. The key here is that material fatigue limits aren’t off-the-shelf numbers—they’re tested under specific conditions, and that brings me to the next critical factor: surface finish.
CNC turning produces a surface, just like any machining process, with tiny imperfections—microscopic grooves, tool marks, and edge burrs. These imperfections are stress risers, meaning they concentrate stress at those points, acting like tiny crack starters. I’ve seen this firsthand: a customer who used a low-quality tool on a 4140 shaft, leaving a rough surface finish (Ra 64 or higher), had a shaft fail in just 20,000 cycles when we expected it to last 2 million. When we re-machined that same shaft to a smoother finish (Ra 16), the fatigue life jumped to over 8 million cycles. That’s the power of surface finish. The smoother the surface, the fewer stress risers, the longer the fatigue life. It’s that simple, but it’s a detail that’s often overlooked because it adds a little time to the machining process.
Then there’s the matter of heat treatment and secondary processes. Most CNC turned shafts get some kind of heat treatment to boost strength and fatigue performance. For example, carburizing a low-carbon steel like 1018 adds a hard, wear-resistant outer layer while keeping the core tough, which is perfect for shafts that need to handle both rotation and sliding loads (like those in a gearbox). Nitriding is another common process that creates a hard surface with minimal distortion, so you don’t have to re-machine the shaft after treatment. But if you mess up the heat treatment—like over-tempering the steel, or not heating it evenly—you can create weak spots that drastically cut fatigue life. I always tell customers that skimping on heat treatment is like skipping the foundation for a house; it might hold up for a while, but it will eventually collapse.
Now, let’s get to the actual numbers. This is where things get tricky, because fatigue life isn’t a fixed value. It’s a statistical range based on load, cycle frequency, temperature, and even the environment the shaft is operating in. The standard way to measure this is through S-N curves (stress vs. number of cycles), which are generated from thousands of test cycles on specialized fatigue testing machines. For a typical 0.5-inch diameter CNC turned shaft made from quenched and tempered 4140 steel, polished to a Ra 16 surface finish, the S-N curve will show that at a stress of 20,000 psi, you can expect roughly 10 million cycles before failure. At 25,000 psi, that drops to around 1 million cycles. At the fatigue limit of 32,000 psi, it will never fail, no matter how many cycles.
But wait—what if that shaft is operating in a high-temperature environment? Like inside a furnace, or near an engine that runs at 300 degrees Fahrenheit? The fatigue limit of steel drops as temperature rises. At 500 degrees F, 4140’s fatigue limit is down to about 25,000 psi, and at 800 degrees F, it’s around 18,000 psi. Add in corrosion from moisture or chemicals, and you’ve got another stress factor. Corrosion creates tiny pits in the surface, which are even worse stress risers than tool marks. I once worked with a customer in the food processing industry who was using 303 stainless shafts that kept failing in 6 months. The problem? The acid in the cleaning solution was creating corrosion pits, cutting fatigue life by 70%. We switched them to 316 stainless and added a passivation process, and their failure rate dropped to zero.
Another big factor is stress concentration from the shaft’s design. CNC turned shafts aren’t just straight cylinders—they have shoulders, keyways, holes, and grooves for set screws or bearings. Every time you change the diameter of the shaft (a shoulder), or cut a keyway, you create a sharp corner where stress concentrates. A sharp corner can increase stress by a factor of 3 or more, which means fatigue life is cut to a fraction of what it would be with a rounded, blended corner. I always advise customers to add generous radii to these features—even if it means a tiny bit more machining time. A 0.030-inch radius at a shoulder on a 4140 shaft can double its fatigue life, easy. I’ve had customers insist on sharp corners to save a few cents, and then come back to me when their shafts fail prematurely, asking how to fix it. It’s a lesson that’s expensive to learn, so I try to teach it early.
Now, you might be wondering: as a CNC turned shafts supplier, how do I actually apply all this to what I deliver? It’s not just about quoting a fatigue life number and calling it a day. Every shaft I supply is made to order, so I work closely with customers to match the material, surface finish, and design to their specific load requirements. For example, if a customer needs a shaft for a robotic arm that will be under 15,000 psi of repeated load, will make 10 million cycles over 5 years, and needs to be corrosion-resistant, I’ll recommend a 0.5-inch diameter 4140 shaft with a Ra 16 surface finish, a 0.030-inch radius at all shoulders, and maybe a light nitride treatment if they need extra wear resistance. I’ll test a prototype of that shaft for fatigue before I send it into production, because I don’t want my name on a part that fails.
I also stay on top of new materials and processes. A few years ago, we started working with a new micro-alloy steel that has a fatigue limit about 15% higher than 4140, with better machinability, so it cuts production time too. For customers who need ultra-high fatigue life, we now offer shot peening— a process where tiny metal balls are shot at the shaft’s surface, creating compressive stresses that actually counteract the tensile stresses that cause cracks. Shot peening can double or triple fatigue life, and it’s become one of my most popular value-added services, especially for aerospace and medical customers.
But here’s the thing: no matter how good the material, how smooth the surface, or how precise the machining, there’s no way to give a universal fatigue life number for a CNC turned shaft. It’s always dependent on the application. A shaft that works great in an agricultural tractor might fail in a medical device because the load is different, the environment is different, and the cycle frequency is different. That’s why I never give a generic “fatigue life of X years” answer. Instead, I ask questions: How much load is the shaft under, repeatedly? How many cycles will it make in its lifetime? What’s the operating temperature and environment? What’s the design of the shaft, including shoulders, keyways, and other features? Once I have those answers, I can work with my team to specify the right material, finish, and processes to meet or exceed the required fatigue life.
I also educate my customers on this, because I’ve seen too many people make the mistake of assuming a shaft is just a shaft. Last year, a customer came to me with a shaft he’d been buying from a competitor, claiming that it was failing in just 3 months, way before its supposed fatigue life. When he sent me the old shaft, I measured it: it was made from 1018 carbon steel, machined to Ra 125 surface finish, with sharp shoulders. The competitor had quoted a “fatigue life of 5 years” based on generic material specs, but the reality was that the shaft couldn’t handle the load the customer was putting on it. I quoted him a re-engineered shaft made from 4140, Ra 16, with blended radii, and since he switched, he hasn’t had a single failure. That’s the difference between a supplier who just sells parts and one who understands the engineering behind them.
At the end of the day, fatigue life for CNC turned shafts is a combination of science, experience, and attention to detail. It’s not about picking a number out of a catalog—it’s about matching every variable to the specific needs of the application. As someone who’s been doing this for over a decade, I’ve seen the costs of getting it wrong, and the benefits of getting it right. I’ve seen manufacturing lines shut down because of a single failed shaft, and I’ve seen customers sleep easier knowing their parts will hold up for the long haul.
If you’re working on a project that depends on CNC turned shafts, and you want to make sure the fatigue life is exactly what you need, don’t just go with the cheapest quote. Reach out, tell me about your application, and let’s work together to engineer a shaft that will perform reliably for its entire lifespan. I’m not just here to sell you a part—I’m here to make sure your machinery runs smoothly, safely, and without unnecessary downtime.
Aluminum Turned Parts References
- Dowling, N. E. (2012). Mechanical Behavior of Materials. Pearson Education.
- ASM International. (2000). Fatigue Data Book: Ferrous Alloys. ASM International.
- Steven, G. M. (1997). Surface Finish Effects on Fatigue Life of Machined Steel Components. Journal of Manufacturing Processes.
- Boyer, R. R. (1996). Atlas of Fatigue Curves. ASM International.
- Trent, E. M., & Wright, P. K. (2000). Metal Cutting. Butterworth-Heinemann.
Huizhou Quanyi Precision Hardware Products Co., Ltd.
Address: Building A10, 7th Floor, Zhongchuangyingke 5G Industrial Park, Zhonghan Industrial Park, Tonghu Town, Huizhou City
E-mail: info@qycncturning.com
WebSite: https://www.qycncturning.com/
