Hey everyone, if you’ve ever worked with custom machined parts—whether for aerospace, medical devices, or even that high-performance car project you’ve been tinkering with—you know that one tiny misstep can derail the entire project. At our precision machining shop, we deal with roundness requirements literally every single day, and let’s be real: it’s not just a “nice-to-have” spec. It’s the line between a part that works flawlessly and one that’s going to cause huge headaches down the line. Today, I want to break down what actually goes into the roundness requirements for precision machined parts, from the basics you might’ve heard before to the specific stuff we as suppliers actually factor in when we’re setting up a job. Precision Machined Parts
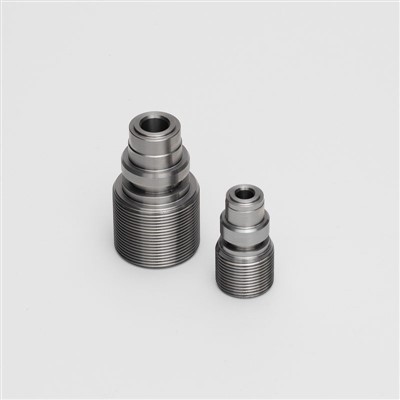
First, let’s get on the same page about what roundness even means. I know, it sounds simple—how “perfect” a circle is, right? But here’s the thing: it’s not just “how round it looks under a microscope.” The official definition from standards bodies like ISO or ASME is the deviation from a perfect geometric circle, measured as the difference between the smallest and largest radii from a central point. So if a part has a radius of 50mm on one side and 50.02mm on the opposite, that’s a roundness deviation of 0.02mm. But that number isn’t random—what matters is why that deviation is critical, and that changes entirely depending on what the part is doing.
Let’s start with the biggest factor that drives roundness requirements: the part’s application. This is non-negotiable. A part for a toy robot is going to have way different specs than one for a heart pump, or a jet engine turbine. For example, if you’re machining a bearing race for a medical pump, even a 0.005mm roundness error might cause friction that leads to the pump failing prematurely. But if it’s a spacer for a garden hose fitting, a 0.1mm deviation is totally fine—no one’s going to notice, and it won’t affect how the hose works. That’s why we never just pull a roundness spec out of thin air; we dig into what the part is being used for first.
Next, there’s the material you’re working with. This is something a lot of first-time clients don’t realize—roundness requirements change depending on if you’re machining aluminum, titanium, plastic, or something harder like tool steel. Aluminum is soft, so it’s way easier to deform during machining. If you’re running a high-speed cut on a thin-walled aluminum tube, the tool pressure might cause the wall to flex, leading to a slight oval shape. Titanium, on the other hand, is stiffer but has a tendency to work-harden, so you have to adjust cutting speeds and feeds to avoid chatter, which can mess with roundness. We’ve had jobs where a client came in with a roundness spec for aluminum, and we had to adjust it slightly because the material they picked was thinner than they thought—otherwise, the part would warp after machining. That’s the kind of thing only a real supplier with hands-on experience catches, not a textbook.
Then there’s the machining process itself. Not all CNC machining operations are equal when it comes to hitting roundness targets. Turning is the most common for round parts, right? When you’re turning a bar stock on a lathe, the main factors here are the lathe’s accuracy, the tool holder rigidity, and how you secure the part (that’s called fixturing, by the way). If you clamp a part too tight, you can actually distort it—so we use soft jaws for final operations to release that clamping pressure once the part is at its final diameter. For parts that require milling, like odd-shaped components with multiple round features, we have to use 5-axis machining sometimes, and the roundness of each feature depends on how well the machine’s axes are calibrated. We do daily checks with a calibration ball to make sure our CNCs are on point, because even a tiny calibration error will throw roundness off.
Wait, also—tolerance stacking! That’s another big one. Roundness isn’t a standalone spec; it has to fit with all the other tolerances on the part. For example, if a shaft has a roundness spec of 0.01mm, but the bearing it fits into has an internal roundness of 0.008mm, you can’t just mix those—they won’t mate properly. We work closely with our clients to make sure all their tolerances align, so we don’t end up with a part that’s machined to spec but doesn’t fit with the rest of their assembly. That’s probably the most frustrating thing for both sides: spending time and money on a part that meets your spec, but fails because of a tolerance mismatch.
Let’s talk about how we actually measure roundness, because the measurement method affects the requirement too. A lot of shops might use a dial caliper, but that’s super basic and only gives diameter measurements at a few points. To get accurate roundness readings, we use a roundness tester— it spins the part while a probe measures hundreds of points, mapping the exact deviation. For high-precision parts, we might even use coordinate measuring machines (CMMs) with contact probes that scan the entire surface. The key here is that the measurement method has to be accurate enough for the spec. If a part requires roundness to 0.001mm, using a caliper is useless—you need that specialized equipment. We always communicate to our clients how we’ll be measuring the part, because if we use a different method than their quality team, you can get conflicting results.
Also, environmental factors during machining and inspection. I know this sounds trivial, but temperature changes can wreak havoc on roundness. If we’re machining a part in a shop that’s 25°C, then moving it to an inspection area that’s 35°C, the metal expands, and suddenly the roundness reading is off. We have climate-controlled inspection rooms for critical parts, and we make sure parts are at room temperature before measuring. We also don’t machine parts too early if they’re going to sit in a hot warehouse for a few days— that’s a simple step, but it’s one that prevents so many quality issues.
Let’s throw in a real example to make this concrete. Last year, we had a client who needed precision machined valve balls for a natural gas control system. Their initial spec was roundness of 0.003mm, but when we ran a test part, we found that their manufacturing process for the valve seat only could hold roundness to 0.005mm. We told them upfront that holding 0.003mm on the valve ball would be a waste of money—our process could do it, but it would add 30% to the cost, and it wouldn’t improve the performance because the seat couldn’t match that accuracy. We adjusted the spec to 0.005mm, and they saved a bunch of cash while still getting a part that worked exactly as intended. That’s the kind of collaborative approach we take, not just saying “we can meet your spec” regardless of whether it’s necessary.
Another example: we had a medical device client making surgical tool handles. They were using a 3D printed prototype that had a rough roundness, so they transferred that spec to the machined part. When we machined the first few parts, they came in at roundness of 0.02mm, but when the client tested the prototype, it felt “off” in their hand. Turns out the 3D printed part had a rough surface finish that masked the roundness deviation. Once we explained that, they adjusted the roundness to 0.01mm, and the final parts felt perfect, and passed all their biomechanical tests. That’s why we always encourage clients to test prototypes first, and work with us to refine specs—we’re not just machine operators, we’re problem solvers.
Wait, let’s also address a common misconception: roundness is the same as cylindricity. No, totally different. Roundness is for a single cross-section of a part (like a slice of a shaft), while cylindricity accounts for the entire length of the part— so it checks both roundness at every cross-section and how straight the axis is. That’s a mistake we see all the time: clients mix those two specs up, and end up with a part that’s round at one point but tapered along the length, which is useless for applications like hydraulic cylinders. We always clarify that with our clients to make sure we’re machining exactly what they need.
Now, for the practical stuff—what do you need to do if you’re a client setting roundness requirements for precision machined parts? First, tell us exactly what the part is doing, and what components it’s mating with. Don’t just say “roundness 0.01mm”—tell us it’s a bearing race for an electric motor, or a valve ball for a gas line. Second, be honest about your budget and timeline. Tighter roundness specs mean more machine time, more calibration checks, sometimes more material waste, so there’s a cost tradeoff. Third, work with your quality team to confirm the mating parts’ specs, so we can make sure everything aligns.
At the end of the day, roundness is all about function over form. It’s not about having a “perfectly round” part for the sake of it—it’s about having a part that does what it’s supposed to do, reliably, every time. That’s why our team spends so much time going through these factors with every client, even if it means adjusting specs slightly to get a better final product.

If you’re working on a project that needs precision machined parts with tight roundness requirements, we can help. Our team has years of experience across aerospace, medical, automotive, and industrial applications, so we can walk you through every step of setting the right roundness spec, machining the part accurately, and verifying it to your standards. Just reach out to our team to start a conversation about your project—we’re here to answer questions, adjust specs, and make sure you get the parts you need, on time and on budget.
Precision Disc Parts Machining References
ASME Y14.5-2018, Dimensioning and Tolerancing
ISO 12180-1:2011, Geometrical Product Specifications (GPS) – Cylindricity – Part 1: Vocabulary and Parameters
Machining Fundamentals: Precision Roundness and Cylindricity, Modern Machine Shop, 2022
Taizhou Liuhuan Machinery Co., Ltd.
As one of the most professional precision machined parts manufacturers and suppliers in China, we’re featured by quality products and good service. Please rest assured to buy customized precision machined parts made in China here from our factory. For quotation, contact us now.
Address: Xinyuan Industrial Zone, Damaiyu Street, Yuhuan City, Zhejiang Province,China
E-mail: tzlhmachining@gmail.com
WebSite: https://www.tzlhmachining.com/
